Health Chi-Tech
Choosing the right Drill Bits can turn a rough hole into a clean, accurate cut—or leave you with a scorched edge and a broken tip. The best choice depends on more than the drill itself. Material, hole size, bit design, and working speed all matter. A bit suited to soft pine may struggle in stainless steel, while masonry needs a different cutting edge altogether. Small details count.
As tooling specialist [expert name to verify] puts it, “Match the bit to the material, and let the cutting edge do the work.” Please verify the expert’s name and wording before publication; an unverified quotation should not be presented as a real attribution.
This guide offers ten practical tips for choosing Drill Bits for common jobs around the workshop, home, and job site. It covers materials such as wood, metal, and masonry, along with shank compatibility, coatings, bit sizes, and signs of wear. You’ll also see why a sharp, correctly sized bit often matters more than buying the most expensive set. Check the manufacturer’s guidance, secure the workpiece, and start at a sensible speed. Feel the cut. If the bit wanders, overheats, or produces ragged edges, pause and reassess. One honest caveat: no checklist replaces experience with the exact material in front of you.
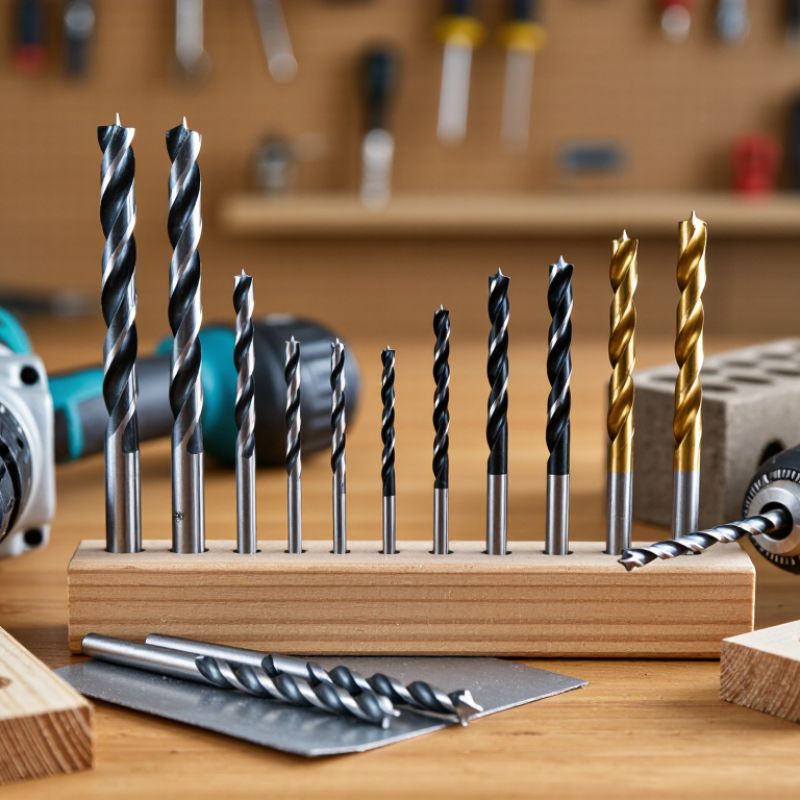
Choosing the right drill bit starts with the workpiece, not the drill itself. High-speed steel, or HSS, suits wood, plastic, and mild steel. It is affordable and easy to sharpen. I use HSS for occasional household repairs and small metal holes. Keep the speed moderate, and apply cutting fluid when drilling steel.
Cobalt bits contain an alloy that handles more heat than standard HSS. They work well on stainless steel, hard steel, and repeated workshop jobs. Use steady pressure instead of forcing the bit. Excessive pressure can dull the cutting edge quickly. Carbide bits are harder and more heat-resistant, making them useful for masonry, tile, cast iron, and abrasive materials. However, carbide is brittle. A sideways twist can chip the tip. I once damaged a carbide bit by rushing a misaligned hole, so patience matters more than expected.
Tips: Match the bit diameter to the fastener or hole specification. Check the package for suitable materials. Use a pilot hole for larger diameters. Let the bit cut; do not push until it squeals. For stainless steel, keep the bit moving slowly and use lubricant. Inspect the tip under good light before each job. A worn edge may still drill wood, but it can wander on metal. My own selection is not always perfect, especially when materials are coated or layered. When uncertain, test on a hidden area and monitor heat, chips, and cutting sound.
Select the bit material according to the workpiece, heat generation, machine stability, required tool life, and drilling environment. The recommendations below describe typical applications; the exact result also depends on bit geometry, diameter, point angle, speed, feed, and coolant.
| Tip | Selection Factor | HSS (High-Speed Steel) | Cobalt HSS | Carbide |
|---|---|---|---|---|
| 1 | Identify the workpiece | Suitable for general-purpose drilling in mild steel, low-alloy steel, aluminum, brass, copper, wood, and many plastics. | Preferred for stainless steel and heat-resistant alloys that generate more heat and work-harden during drilling. | Best suited to abrasive materials, cast iron, hardened workpieces, composites, and high-volume production when the setup is rigid. |
| 2 | Match hardness and heat resistance | Provides a balanced combination of hardness, toughness, and ease of sharpening, but loses hardness sooner when overheated. | Usually contains approximately 5–8% cobalt, increasing hot hardness and wear resistance compared with standard HSS. | Has substantially greater hardness and wear resistance than HSS, retaining cutting ability at higher temperatures, but is more brittle. |
| 3 | Consider stainless steel | Can drill stainless steel when sharp, properly lubricated, and operated at conservative speed, but may wear faster. | Typically the most practical choice for repeated stainless-steel drilling because it tolerates heat and work-hardening better. | Can perform well in production applications, but requires accurate alignment, adequate rigidity, and the correct geometry to reduce edge chipping. |
| 4 | Evaluate machine rigidity | More forgiving of hand-held drills, interrupted cuts, vibration, and minor alignment errors. | More demanding than standard HSS but still reasonably tolerant of normal workshop conditions. | Requires a rigid machine, secure workholding, and minimal runout because vibration or impact can fracture the cutting edge. |
| 5 | Control drilling heat | Use a suitable cutting fluid and avoid excessive speed or pressure to prevent tempering and premature dulling. | Handles heat better than standard HSS, but cutting fluid and chip evacuation remain important for long tool life. | Often permits higher cutting speeds, but avoid thermal shock and follow the tool maker’s guidance on dry or lubricated cutting. |
| 6 | Account for abrasiveness | Economical for ordinary metals but wears relatively quickly in abrasive composites, glass-filled plastics, and similar materials. | Offers better wear resistance than HSS and may be suitable for moderately abrasive materials when the geometry is appropriate. | Generally the strongest choice for abrasive workpieces because carbide resists abrasive wear far better than steel-based bits. |
| 7 | Choose the right operating speed | Normally requires the lowest cutting speed of the three materials, especially in hard or heat-sensitive metals. | Usually supports higher cutting speeds than standard HSS in difficult alloys, subject to diameter, workpiece, and coolant conditions. | Can support the highest cutting speeds in suitable rigid setups, but excessive feed, vibration, or interrupted cutting can cause edge failure. |
| 8 | Plan for sharpening and maintenance | The easiest and least costly of the three to resharpen with common workshop grinding equipment. | Can be resharpened similarly to HSS, although cobalt-containing steel may require careful grinding to avoid overheating. | Normally requires specialized diamond grinding equipment; carbide edges should not be treated like ordinary steel bits. |
| 9 | Balance toughness and edge life | Best when toughness, versatility, lower purchase cost, and tolerance of occasional misuse are more important than maximum life. | Provides a strong compromise between toughness and extended edge life for demanding metalworking tasks. | Delivers the longest wear life in stable, repetitive applications, but its lower toughness increases the risk of chipping or breakage. |
| 10 | Make the final selection | Choose HSS for general maintenance, mixed materials, portable drilling, and cost-effective everyday work. | Choose cobalt HSS for frequent drilling in stainless steel, tougher alloys, or applications where standard HSS dulls too quickly. | Choose carbide for abrasive, hardened, or high-volume work when the machine, workholding, alignment, and cutting parameters are well controlled. |
Practical rule: use standard HSS for versatility, cobalt HSS for heat-producing difficult metals, and carbide for maximum wear resistance in rigid, controlled setups. Always verify the recommended speed, feed, point geometry, and coolant requirements for the specific bit and workpiece.
HSS works well for wood, plastic, and mild steel. Cobalt handles stainless and harder steels. Carbide suits masonry, tile, and cast iron. Check the bit package, especially for coated or layered materials.
Use a slower speed, steady pressure, and cutting fluid. Let the bit cut without forcing it. If smoke or squealing starts, stop and reassess.
A 118° point suits general work, including wood, plastic, aluminum, and mild steel. A 135° point often works better on harder metals. It is not a guarantee; bit design and material thickness matter too.
A small dimple helps keep the bit from skating across a clean, flat surface. I still find it easy to rush this step.
Match the hole specification using the correct fractional, metric, or number-gauge chart. For example, 3/8 inch is 0.375 inch, while 9.5 mm is slightly smaller than 9.525 mm.
No. A larger gauge number means a smaller bit. No. 80 is about 0.0135 inch; No. 1 is about 0.2280 inch. Check the chart carefully.
Use one for larger diameters, and match the final bit to the required hole size. A test hole in scrap can help reveal problems.
Squealing, smoke, rubbing, or unusually hot metal are warning signs. Short, controlled chips are often a better sign. Pause, inspect the tip, and check speed, pressure, and cooling.
Choosing the right Drill Bits starts with matching the bit material to the workpiece. High-speed steel bits suit many general-purpose tasks, cobalt bits are better for tougher metals, and carbide bits are designed for very hard materials. The point angle also matters: a 118-degree point works well for general drilling, while a 135-degree point can help the bit start more effectively in harder metals. Select the size from a fractional, metric, or number-gauge chart, and check that the shank fits your tool.
Before drilling, confirm that the bit type and length suit the tool, hole depth, and material. Use the manufacturer’s speed and feed recommendations as a starting point, adjusting for the workpiece and bit material. Larger bits generally require lower RPM than smaller ones. Taking time to match these details can improve accuracy, reduce unnecessary bit wear, and help produce cleaner, more consistent holes.